 MORRGARY
Home / Craft
Three crafts, one standard: made in our own plant
Hot pressing, surface finishing and laser cutting all happen in-house in Nanxun, Huzhou — a region known as one of China’s wood flooring capitals. Owning the process is what keeps the fit accurate, the weight low and the surface durable.
01 · Core Panel
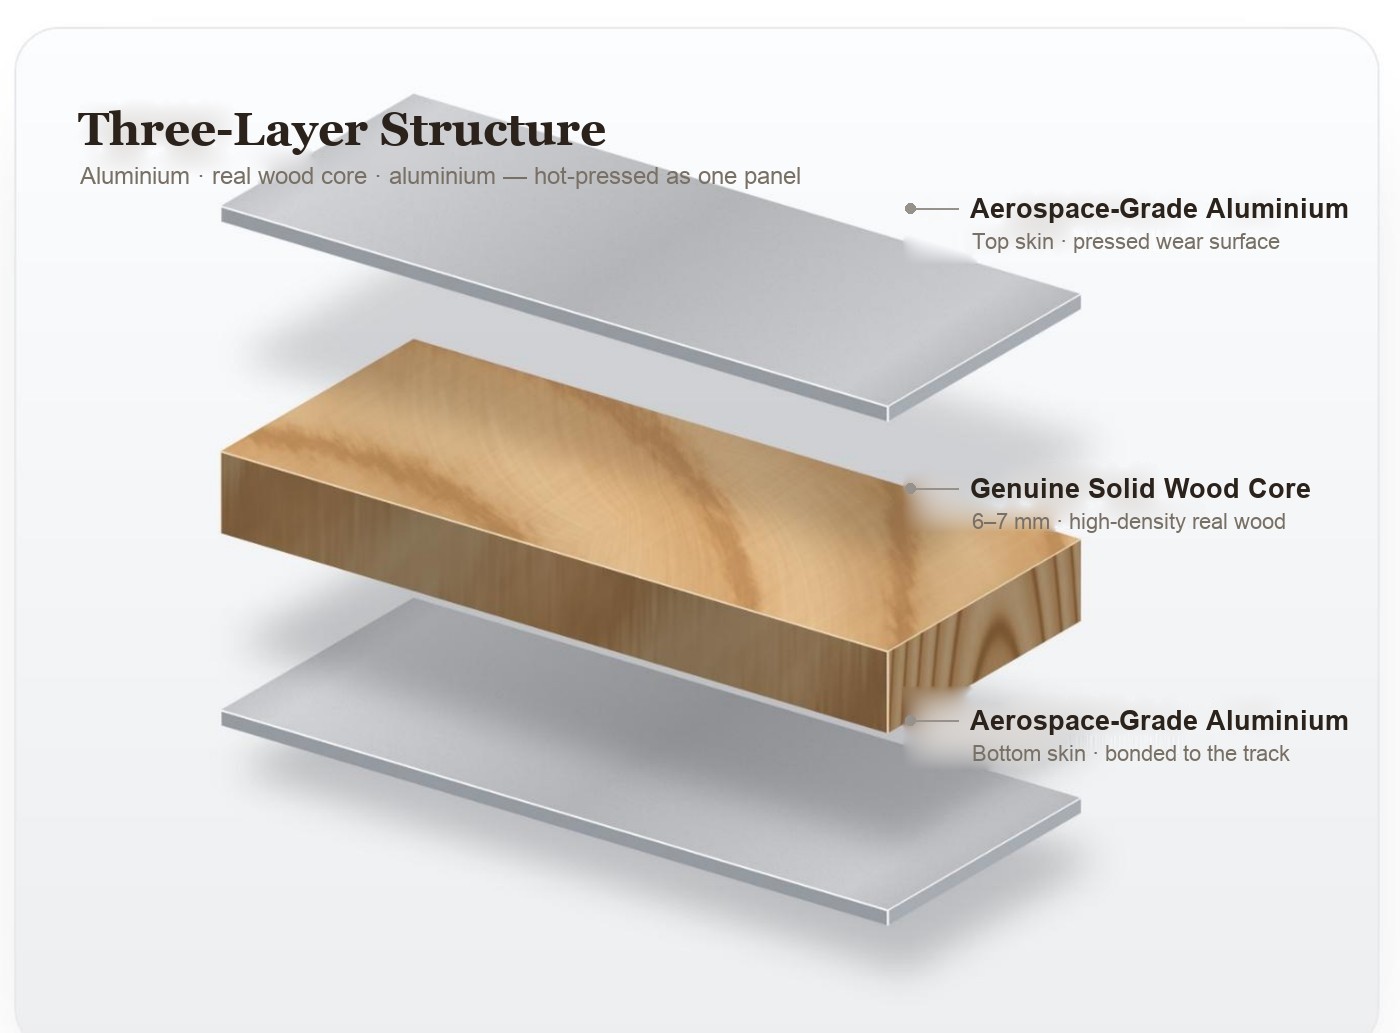
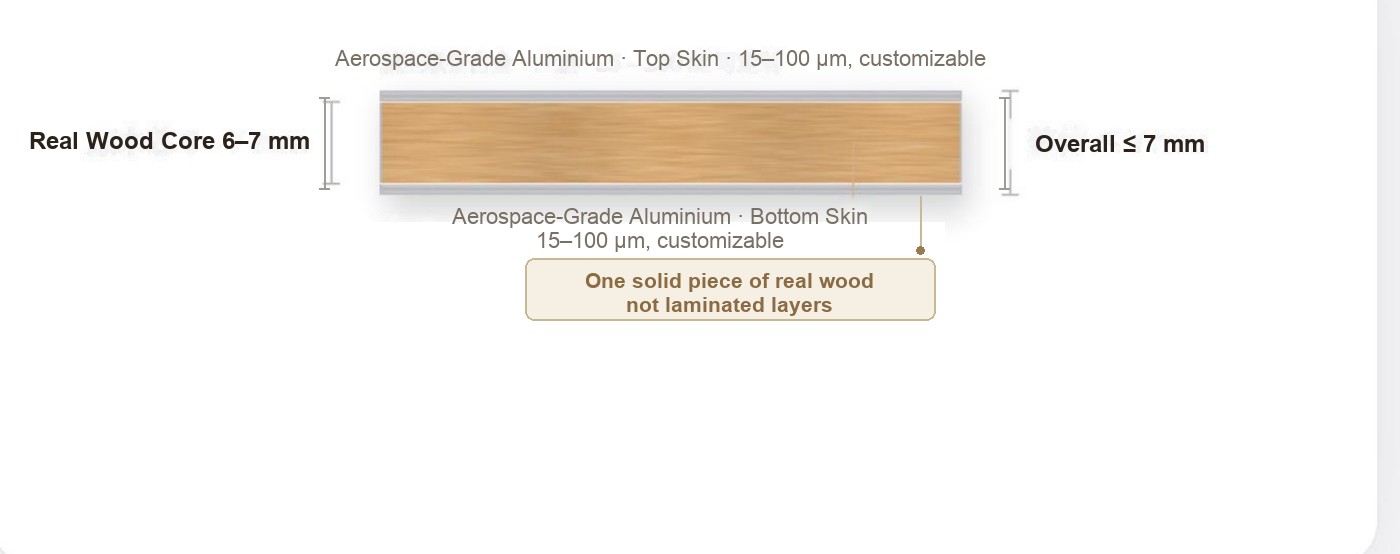
Aluminium–wood–aluminium, pressed in one cycle
The main panel is not a laminate of glued layers. Aluminium sheets above and below a genuine solid wood core of 6–7 mm are hot-pressed together in a single cycle on a 3.2 m × 1.8 m press. The core is real wood — cut a panel open and you see wood, not print. At equal thickness the panel is around 59% lighter than a conventional construction, and total thickness stays at 7 mm or less.
- 3.2 × 1.8 mHot-press platen for full-size panels
- ≤ 7 mmTotal panel thickness
- 6–7 mmSolid wood core
- −59%Weight vs conventional panel, equal thickness
02 · Hidden Track
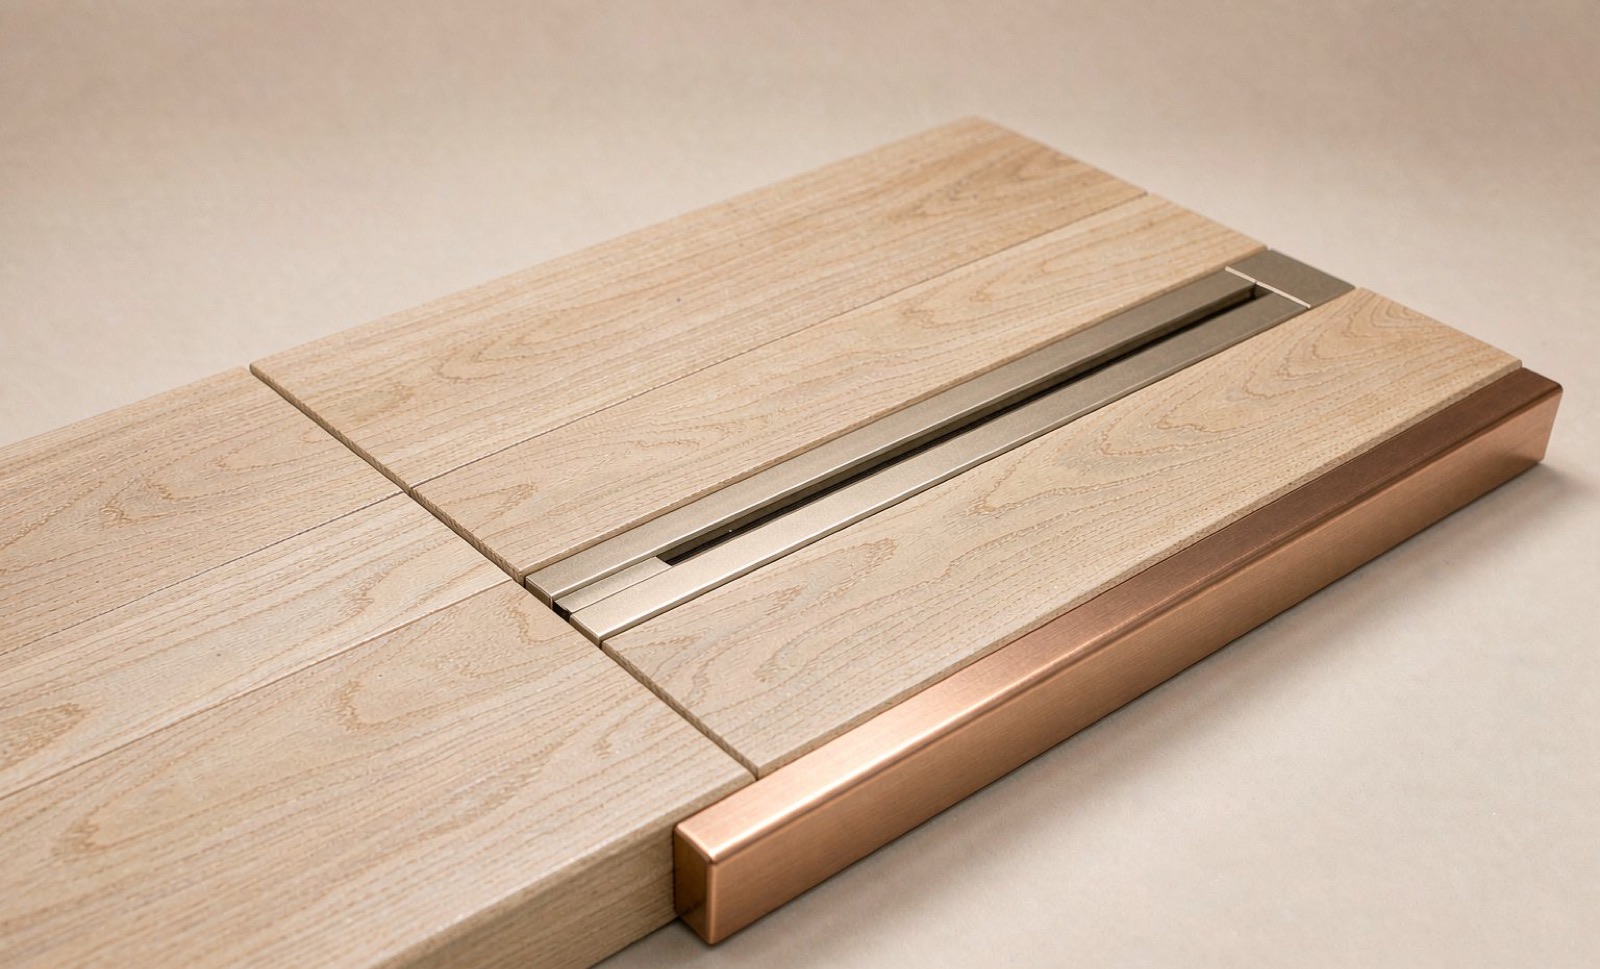
Fourth-generation integrated track — nothing visible, nothing loose
Conventional floor systems add visible clips, strips and screws. Ours integrates the track into the panel itself as a one-piece aluminium profile on the underside: the surface stays clean after installation, the original floor is never removed, and the number of loose fittings drops by around 40% — which is where rattles and lost parts usually come from.
- 0Visible track parts after installation
- −40%Loose fittings vs conventional track systems
- No drillingOriginal floor and body stay untouched
- 24 hAfter-sales response if anything needs attention
03 · Diamond-Rock Surface
Pressed to 16,000 revolutions — with real grain depth
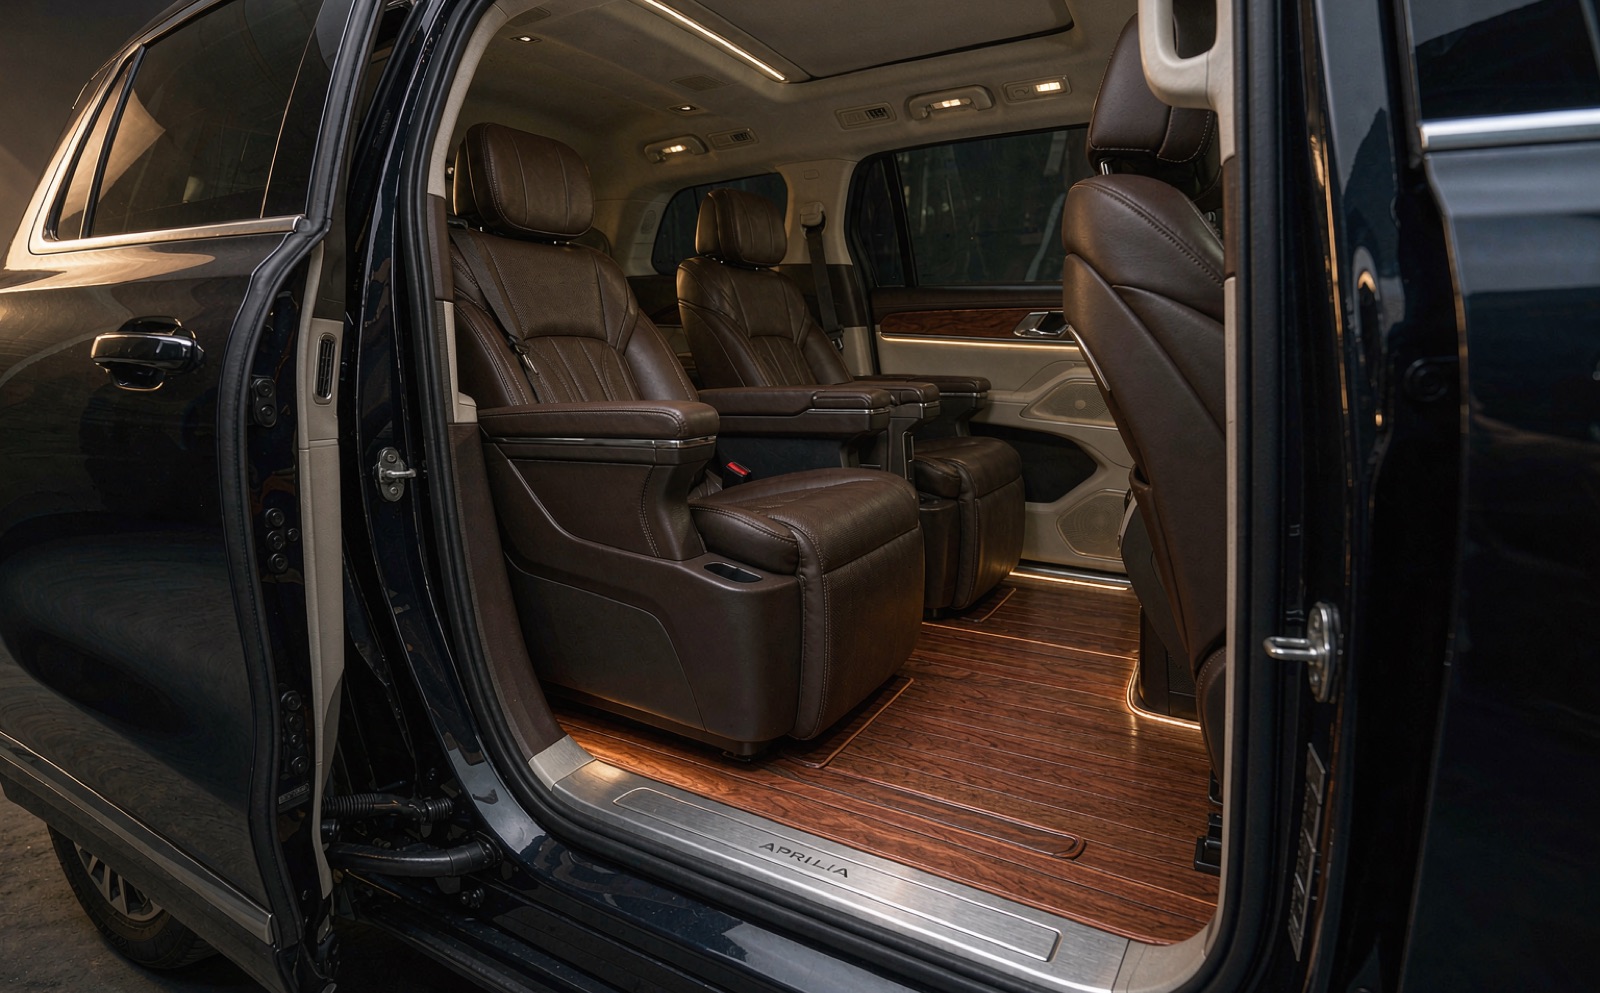
UV-printed floors typically score around 3,000 revolutions on the standard abrasion test. Our Diamond-Rock surface is a pressed wear layer rated to 16,000 — roughly five times the wear life — and because the texture is pressed rather than printed, the grain has a tactile depth a flat print cannot reproduce. Shoes, luggage and daily use leave less trace.
- 16,000Revolutions abrasion rating
- ≈ 5×Wear life vs typical UV-printed surface (~3,000)
- PressedTactile grain, not a flat print
- Same codeSurface and finish matched per finish code
Production
From order to shipment, inside one plant
Every step below happens in our own 6,000 m² facility in Nanxun — nothing critical is outsourced.
| Stage | What happens |
|---|---|
| 1 · Order & configuration | Vehicle pattern, finish code and kit components confirmed with you before production starts. |
| 2 · Panel engraving & printing | Aluminium skins are engraved and the coded finish is applied by UV flatbed printing. |
| 3 · Surface finishing | Membrane-press paint line (2.4 m) and roller-coating line (1.6 m) build the Diamond-Rock wear surface. |
| 4 · Hot-press lamination | Aluminium skins and the solid wood core are pressed into one panel. |
| 5 · Laser cutting & shaping | Pattern-specific contours cut by laser to the 3D-scan geometry; five-axis profiling for shaped parts. |
| 6 · Three-stage inspection | In-process sampling at key stages plus a final accessory check before packing — pattern accuracy, finish and completeness. |
| 7 · Packing & dispatch | Export-grade packing; each kit is traceable by its own code. |
Capacity is around 100 kits per day (roughly 3,000 per month) on this line, which is what allows us to serve both individual owners and volume orders for dealers and fitment shops.
See it on your vehicle pattern
Pick a finish, confirm the kit, get a quote — the process starts with your model.